русский
 عربى
A 0.6 mm inside corner in a hardened H13 mold insert forces a small end mill into 52 HRC steel, and that is a tool-breaking job most shops would rather decline. EDM discharge machining sidesteps the ...
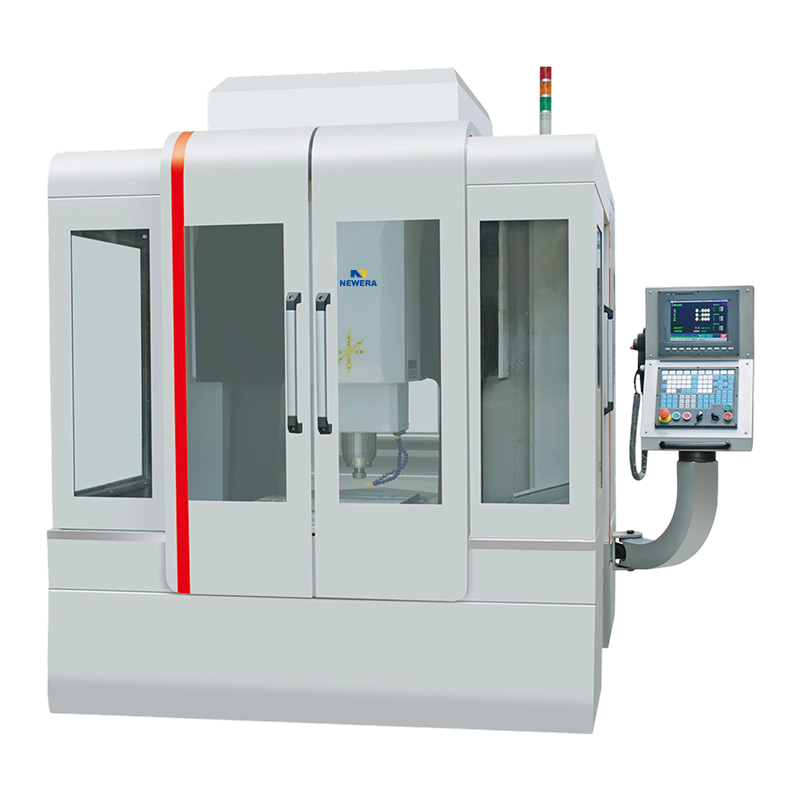
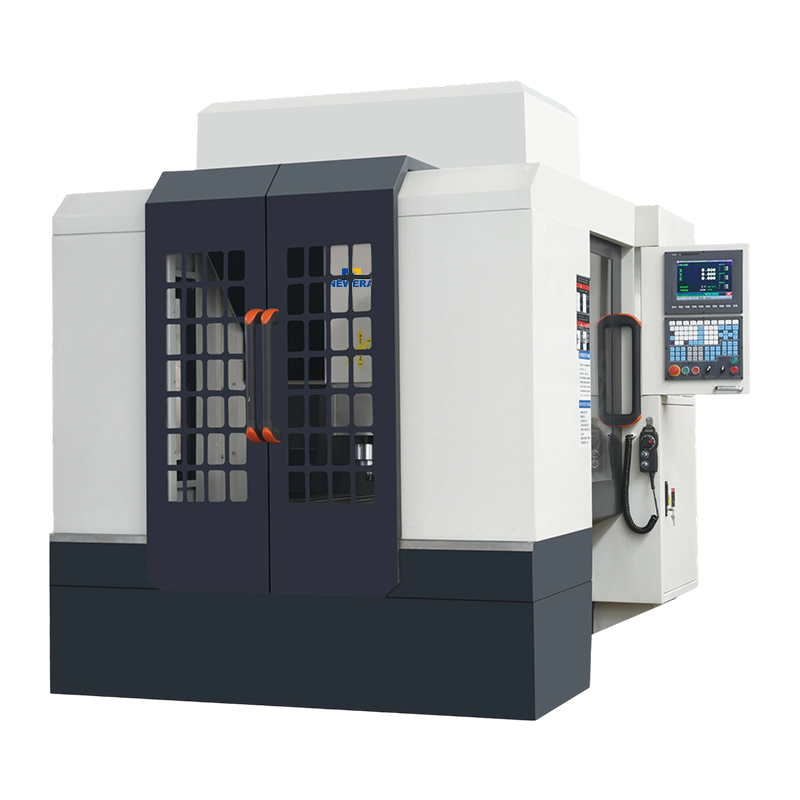
CNC Gantry Machine
Home / Products / Engraving and Milling Machine / CNC Gantry Machine / NE1090 CNC Gantry Milling Machine
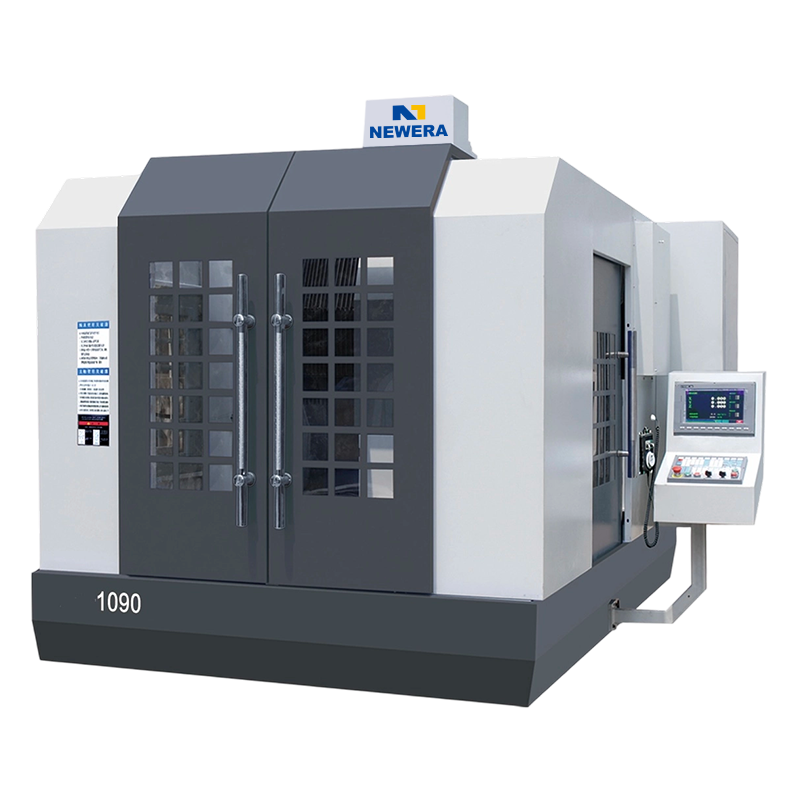
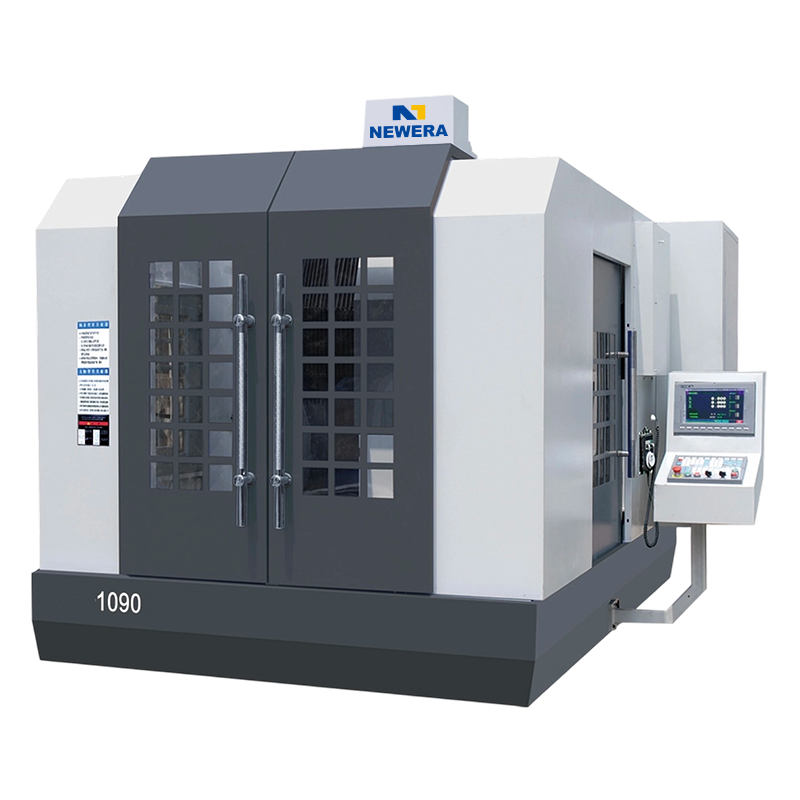
Model: NE1090
NE1090 CNC Gantry Milling Machine
Contact us
- Details
- Technical Parameters
- Contact Us
ABOUT US
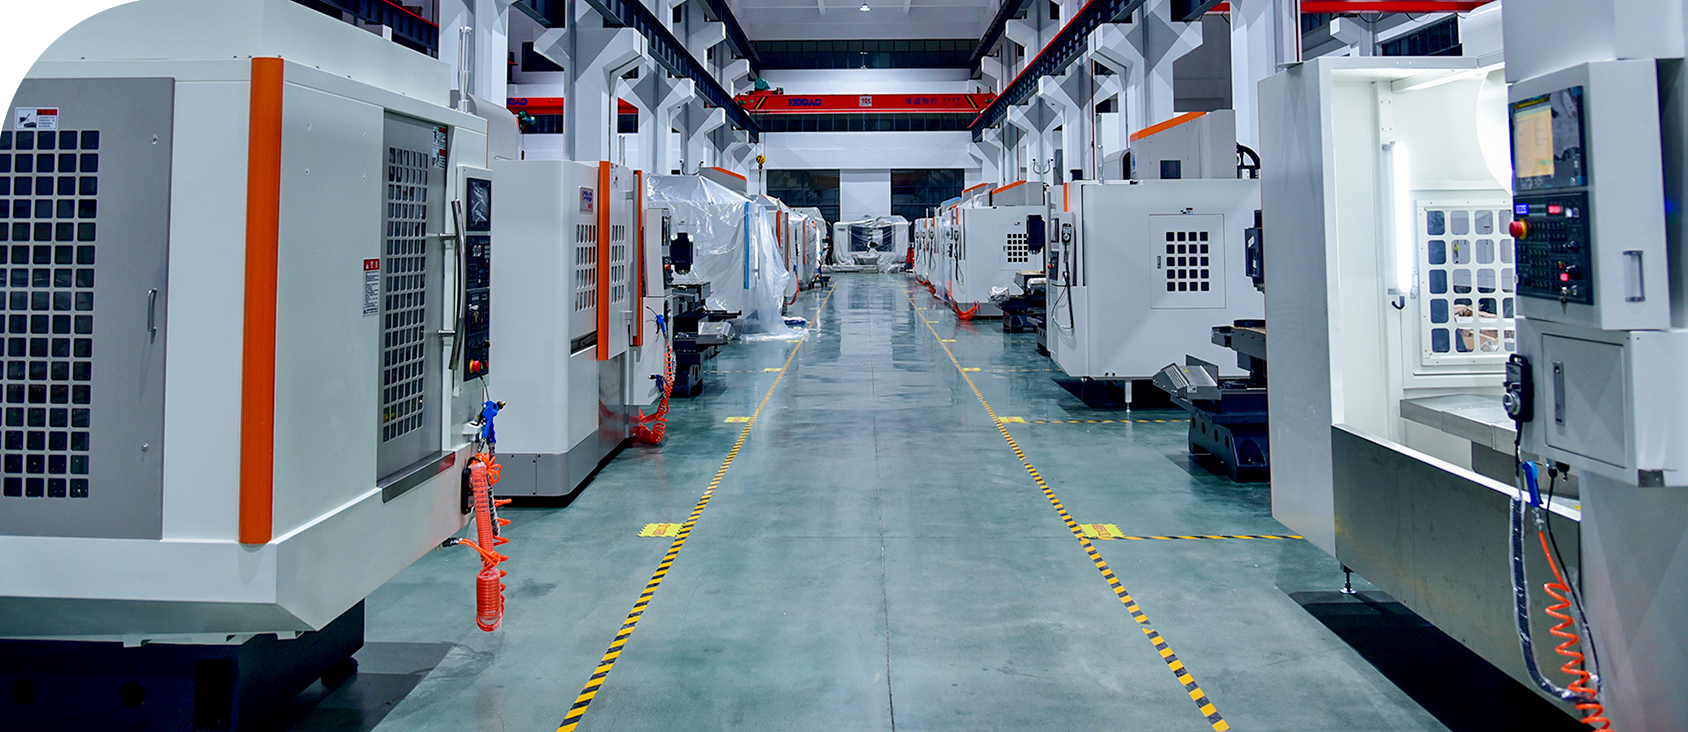
Nantong New Era Technology Co., LTD
Nantong New Era Technology Co., LTD specializes in developing, designing and producing numerical control machine and CNC machine tool for more than 20 years. We have a professional team in technology development, manufacturing and sales services.
As a professional OEM NE1090 CNC Gantry Milling Machine manufacturers and ODM NE1090 CNC Gantry Milling Machine company, New Era has continuously obtained the advanced scientific and technological achievements at home and abroad, and has now developed into a professional manufacturer with a complete production and mounting center.We always provide customers with the best solutions and creates the maximum value with high-quality products and perfect services.
As a professional OEM NE1090 CNC Gantry Milling Machine manufacturers and ODM NE1090 CNC Gantry Milling Machine company, New Era has continuously obtained the advanced scientific and technological achievements at home and abroad, and has now developed into a professional manufacturer with a complete production and mounting center.We always provide customers with the best solutions and creates the maximum value with high-quality products and perfect services.
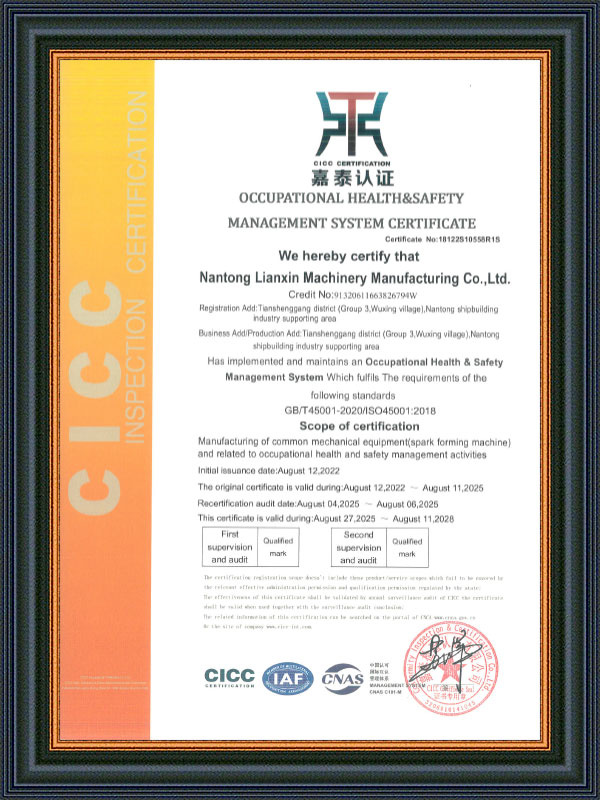
HONORARY CERTIFICATION
CERTIFICATE
LATEST UPDATES
WHAT'S NEWS
-
EDM Discharge Machining Explained: Process, Tooling and Machine Selection -2026 -10-14
-
What Does EDM Stand For in Machining? Electrical Discharge Machining Explained -2026 -10-07Harden a mold insert to 52 HRC and the milling cutter that shaped it in the soft state stops being an option. The corner radius is 0.3 mm, the rib is 40 mm deep, and the tool simply cannot reach into...
-
A Guide to CNC Machining for Aerospace: Tolerances, EDM and Machine Tool Choices -2026 -09-30A job shop is quoting a titanium bracket: Ti-6Al-4V, 240 mm long, two bearing bores held to ±0.010 mm, a 0.8 mm-wide seal groove that must finish at Ra 0.4 µm, and a first article inspection report d...
-
CNC Machining Centers Explained: Types, Key Specifications, and How to Choose -2026 -09-23A machining contractor once brought us a quotation for 2,000 pump housings with a simple requirement: a ±0.008 mm bore tolerance, documented on every part. The shop's manual mills could hit that numb...
If you are interested in our products, please consult us.
CONTACT DETAILS
Nantong New Era Technology Co., LTD
- Five-star Industrial Park, Chongchuan District, Nantong City, Jiangsu Province, China
- TEL:+86-19851302688
- E-Mail: [email protected]
Products
Quick link
Mobile terminal
Nantong New Era Technology Co., LTD All Rights Reserved. NE1090 CNC Gantry Milling Machine Manufacturer